Factory Acceptance Test (FAT): Key Principles, Processes, and Best Practices

In the industrial production lifecycle, a link directly determines whether products leave the factory qualified and meet customer requirements: the Factory Acceptance Test (FAT). Simply put, FAT is a systematic series of inspections and tests conducted by manufacturers and customers (or their representatives) before products ship. Its primary goal is to verify that a product’s quality, functionality, and safety align with pre-agreed standards.
From large industrial machinery and precision medical equipment to everyday production devices, FAT serves as a non-negotiable step in quality control. This guide breaks down FAT’s core concepts, principles, implementation processes, industry applications, and future trends, providing a clear roadmap for ensuring product reliability before shipment.
Understanding the Basics of Factory Acceptance Test (FAT)
What Is Factory Acceptance Test (FAT)?
Factory Acceptance Test (FAT) is a comprehensive “quality audit” performed after a product is manufactured but before it leaves the factory. Conducted collaboratively by manufacturers and customers (or authorized representatives), FAT verifies that the product meets predefined criteria for functionality, performance, safety, and compliance.
Think of it as a final check before a product “graduates” from the factory. For example, before a new air conditioner ships, manufacturers and dealers test its cooling/heating efficiency, noise levels, and appearance for defects—this is a simplified form of FAT. For industrial products, the process is far more rigorous, but the core objective remains: catch issues before shipment, not after.
Why Is FAT Essential for Manufacturing?
While production-line quality checks are standard, FAT adds a critical layer of verification. Its importance spans both customer and manufacturer interests:
-
Prevents on-site failures:
By identifying defects in the factory, FAT avoids costly delays and rework at the customer’s facility. For instance, imagine a production line machine shipping without FAT, only to reveal mismatched parts during installation—this would disrupt timelines and inflate costs.
-
Builds customer confidence:
Direct participation in FAT lets customers witness product performance firsthand, ensuring alignment with their requirements and reducing the risk of “misrepresented” goods.
-
Drives manufacturer accountability:
FAT forces manufacturers to uphold strict quality standards, improving overall production reliability and reducing post-delivery warranty claims.
-
Comprehensive Coverage with Strategic Focus
FAT should leave no critical component untested, covering functionality, performance, safety, appearance, and documentation. However, it also prioritizes high-risk areas and core functions, allocating more resources to these tests.
Example: Testing a CNC machine involves verifying basic operations but focuses heavily on machining accuracy—its most critical performance indicator.
-
Detailed Documentation and Traceability
Every test result must be recorded meticulously, including timestamps, methodologies, data, and pass/fail outcomes. These records act as a “quality passport,” enabling future issue tracing. All participants must sign off on records to confirm authenticity.
-
Multi-Party Collaboration
FAT is not a one-sided process. Customers (or their representatives) must participate to supervise testing, review data, and address concerns. Third-party inspectors may also be invited to ensure impartiality, reducing post-shipment disputes over quality.
Step-by-Step Implementation of Factory Acceptance Test (FAT)

FAT is a structured process with distinct phases, each designed to ensure thoroughness and clarity.
A. Pre-Test Preparation
Adequate preparation lays the groundwork for successful FAT:
-
Define scope and standards:
Manufacturers and customers collaborate to outline test criteria, pass/fail benchmarks, and excluded items (e.g., on-site installation steps).
-
Assemble the test team:
Include manufacturer engineers (test execution), quality experts (documentation), customer representatives (requirement verification), and third-party inspectors (if needed).
-
Set up the test environment:
Simulate the customer’s on-site conditions with matching power supply, air pressure, and loads. Gather tools (e.g., multimeters, oscilloscopes), documents (test plans, checklists), consumables (lubricants), and safety gear (helmets, gloves).
-
Finalize the test plan:
Detail daily tasks, responsibilities, timelines, and contingency plans (e.g., restart protocols for equipment failures). The plan requires customer approval before execution.
B. Test Plan Design
The test plan acts as a roadmap, outlining:
-
Categorized test items:
Group tests by function, performance, safety, appearance, and documentation. For an industrial oven, this includes heating rate, insulation efficiency, overheat alarms, weld quality, and manual completeness.
-
Test procedures:
For each item, define steps, expected results, and tools. For example, a temperature control test might involve setting 150°C, recording 10 readings, and requiring ≤±2°C deviation (measured via thermocouple).
-
Judgment criteria:
Clarify “pass,” “fail,” and “concession” standards. Minor scratches (≤5mm) might qualify for concession, but a non-functional motor would require immediate rework.
C. Formal Test Execution
With preparations complete, testing begins:
-
Pre-test confirmation:
Manufacturers demonstrate product readiness (e.g., assembly completion, component models) and verify the test environment. All parties review the plan to resolve ambiguities.
-
Real-time testing and documentation:
The team follows test cases, recording raw data (temperatures, pressures) and observations (abnormal noises, alarms). Results are signed by testers and customer reps.
-
Focus on high-risk items:
Critical tests (e.g., sterility checks for medical devices) may require video recording and customer witnessing to ensure traceability.
-
Issue identification:
If non-conformities arise (e.g., excessive vibration), testing pauses, and a “FAT Non-Conformity Report” documents the issue, location, and initial analysis. Irrelevant tests are halted to save resources.
D. Problem Rectification
Addressing issues follows a closed-loop process:
-
Classify defects:
Critical (safety failures, must rectify), major (performance gaps, affects use), and minor (cosmetic flaws, no functional impact). Set deadlines (e.g., 24-hour fixes for critical issues).
-
Root cause analysis:
Engineers diagnose problems (e.g., vibration from misaligned bearings) and propose solutions (e.g., recalibration), approved by the customer.
-
Re-testing:
After rectification, re-inspect the issue. Expand testing if needed (e.g., check overall vibration post-bearing adjustment). Repeat until standards are met.
E. Final Acceptance and Documentation Delivery
Once all tests pass or issues are resolved:
-
Compile the FAT Report:
Include test scope, results, rectification details, and a pass/fail conclusion.
-
Hold an acceptance review:
The team reviews the process, and the customer confirms alignment with requirements.
-
Sign and deliver documents:
The “FAT Acceptance Certificate” approves shipment. Manufacturers provide all records (test plans, raw data, manuals, spare parts lists) for customer reference during installation and maintenance.
Factory Acceptance Test (FAT) Applications Across Industries
FAT protocols vary by product type, with each industry emphasizing unique priorities.
A. Industrial Equipment: CNC Machine Tools
Client Examples of Factory Acceptance Test (FAT) Implementation
A. Case Background
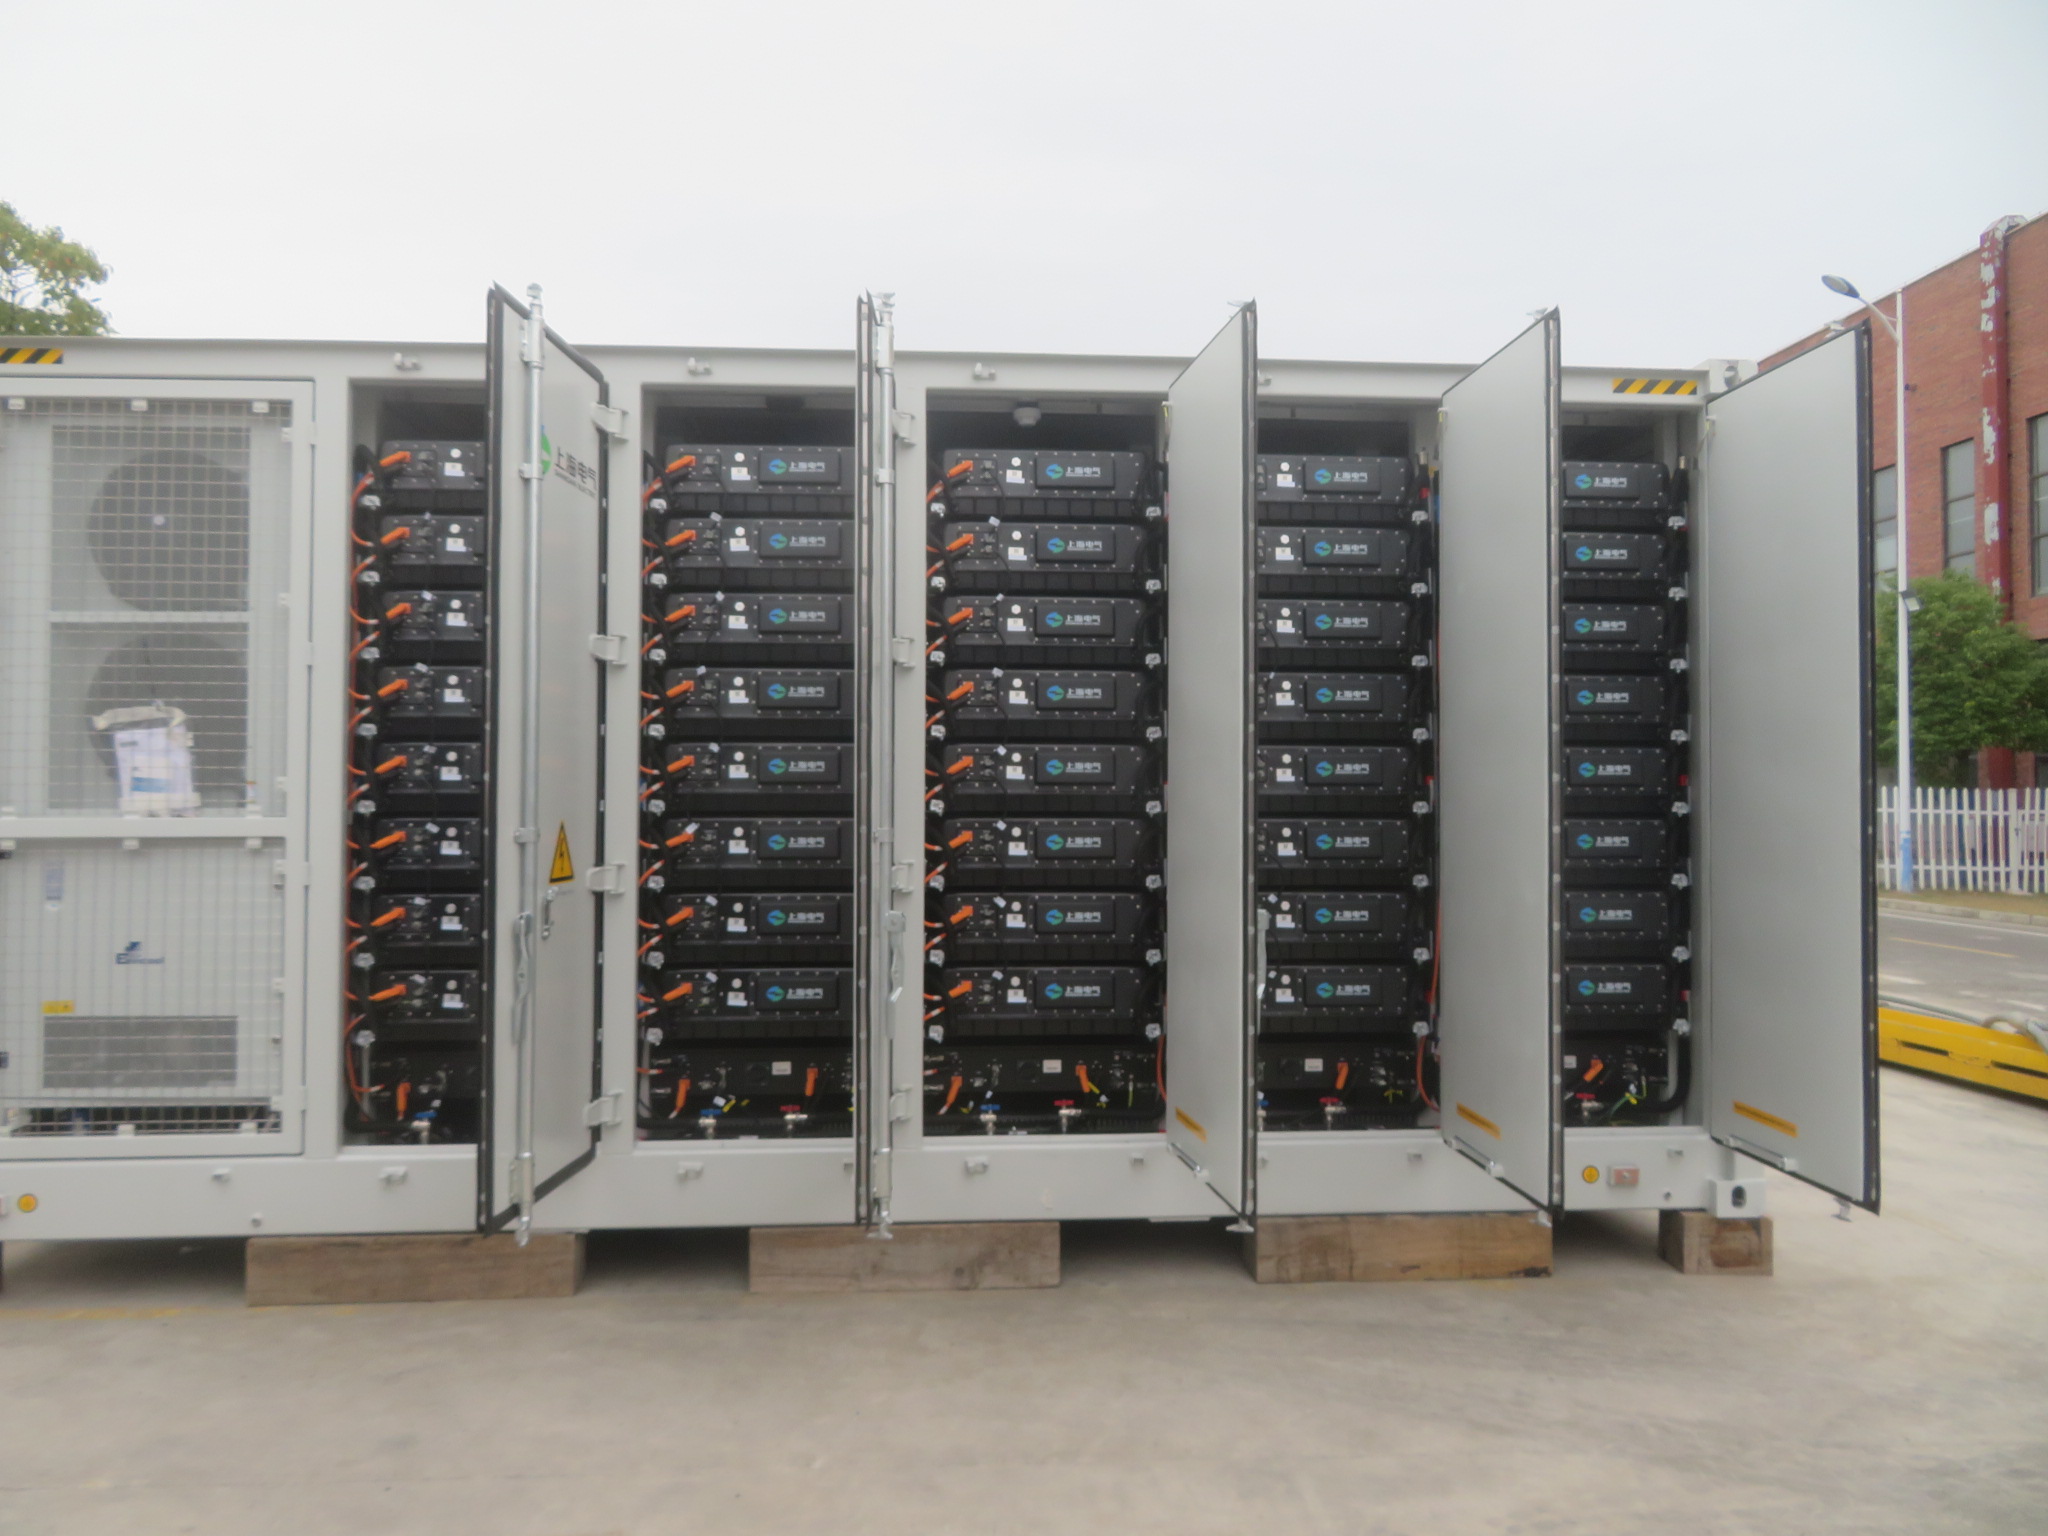
- A customer’s purchased mobile substation equipment required third-party professional inspection and acceptance to ensure compliance with operational standards, as well as to meet the needs of power system expansion and emergency support.
- The inspection was conducted by AQI Service (a third-party inspection company) on March 22, 2025, in accordance with the Inspection and Test Plan (ITP) for mobile substation integration testing.
- Core objective: Verify the functions and performance of each system of the equipment to provide an authoritative basis for its commissioning.
B. Core Inspection Content
-
Scope and Methods
- Inspected Units & Serial Numbers:
- Unit#09 (T250084101050033~T250084101050035)
- Unit#13 (T250084101050049~T250084101050051)
- Unit#14 (T250084101050053~T250084101050055)
- Unit#15 (T250084101050057~T250084101050059)
- Inspection Methods: Visual inspection, final inspection, witness testing, document review
-
Key Test Items & Results
-
Basic Functions (Focus on Unit#14):
- Lighting & sockets: Normal function during distribution vehicle power-on test.
-
- Air conditioner: Auto-switched modes (cooling/heating/ventilation) as required when simulating 16℃ (cooling set) and 25℃ (heating set) conditions.
-
- Fan: Started normally when simulating SF₆ leakage and fire alarm after power-on.
-
Safety Performance:
- Grounding system (Unit#09, Unit#15): No breaks found in visual inspection.
- Grounding continuity (Unit#09): Resistance ≤ 100 mΩ, meeting standards.
-
Power Supply & Control (Unit#13-15):
- Power supply: Stable for distribution, protection panel, GIS (Gas Insulated Switchgear), and transformer.
- Remote control: Sensitive opening/closing of GIS/TGP switches; accurate signal display.
- Current & voltage: Parameters within normal range.
- Transformer: Accurate on-load voltage regulation; timely collection of non-electrical trip/alarm signals.
- Switchgear interlock: Complied with design to prevent misoperation.
-
Communication & Comprehensive Control (Unit#13-15):
- Switch communication: Normal operation; background displayed communication address and equipment status accurately.
- SCADA system: Accurate control of main transformer/HGIS opening/closing via background; correct signal display when simulating faults (light gas, heavy gas, abnormal oil level, etc.).
C. Inspection Results
- All items met requirements; no Non-Conformance Reports (NCR) were issued. Conclusion: “Acceptable”.
- Evidence retention: Photos of testing scenarios (lighting, fan, air conditioner operation, etc.) were taken.
- Data accuracy: Calibration labels of inspection equipment were verified.
- Report compliance: Signed by the inspector and in line with inspection specifications.
Common FAT Challenges and Solutions
Even with structured processes, FAT can face hurdles. Here’s how to address them:
1. Incomplete Test Coverage
Problem: Missing key requirements (e.g., a packaging machine untested for irregular bottles).
Solutions:
- Hold pre-test requirement reviews with customers to confirm all criteria.
- Use FMEA (Failure Mode and Effects Analysis) to identify high-risk areas (e.g., safety functions).
- Implement peer reviews of test cases to catch gaps.
2. Insufficient Customer Participation
Problem: Customers sign off late, leading to disputes over results (e.g., questioning noise test data they didn’t witness).
Solutions:
- Schedule mandatory customer participation for key tests and re-inspections.
- Offer remote access via live video and real-time data sharing (temperature curves, vibration graphs).
- Communicate issues promptly and align on rectification plans during testing.
3. Ambiguous Standards
Problem: Vague criteria (e.g., “smooth operation”) cause disagreements.
Solutions:
- Define quantified standards in technical agreements (e.g., vibration ≤0.02mm).
- Agree on appearance benchmarks (e.g., ≤2 scratches, each ≤3mm) with reference samples.
- Host a pre-test briefing to align on judgment criteria, documented in writing.
4. Delayed Rectification
Problem: Slow issue resolution prolongs FAT (e.g., undiagnosed motor noise causing 3-day delays).
Solutions:
- Prioritize defects with clear owners and deadlines.
- Re-test rectified items with customer witnesses.
- Add 10-20% buffer time in plans for contingencies.
5. Poor Documentation
Problem: Incomplete records (unsigned data, missing root cause analyses) hinder traceability.
Solutions:
- Use a documentation checklist for required records (data, photos, videos) with timestamps.
- Record results in real-time, not post-test.
- Conduct a document audit before acceptance, with missing items resolved first.
How Factory Acceptance Test (FAT) Differs from Other Quality Checks
FAT works alongside other tests but serves a unique role in the quality lifecycle.
-
FAT vs. Site Acceptance Test (SAT)
Emerging Trends in Factory Acceptance Test (FAT)
Intelligent Testing with AI and Automation
AI and automation are enhancing accuracy and efficiency:
- AI-generated test cases: Reduces manual omissions using historical data.
- Real-time anomaly detection: Machine learning identifies patterns (e.g., early bearing failure via vibration data).
- Automated tools: Robots and IoT sensors perform 24/7 unattended testing, with data cloud-uploaded for analysis.
Global Collaboration: Remote FAT and Standard Unification
Global supply chains drive remote FAT adoption, using 5G and IoT for real-time data sharing, reducing travel costs. International bodies (e.g., ISO) are also unifying standards to eliminate cross-border acceptance barriers (e.g., harmonized medical device FATs between the EU and China).
Strengthened Compliance and Traceability
Regulatory demands for safety and sustainability are expanding FAT scope (e.g., carbon emission tests for new energy equipment). Blockchain is increasingly used to encrypt test records, ensuring immutability and credibility.
Conclusion
Factory Acceptance Test (FAT) is the last line of defense against substandard products reaching customers. By following its principles, adhering to structured processes, and adapting to new technologies, manufacturers and customers can ensure product reliability, reduce risks, and strengthen supply chain trust.
In this process, professional third-party organizations like AQI Service can provide neutral and expert support for FAT — from standardized guidance in test plan formulation, to objective verification during on-site execution, and precise analysis of digital test data. These services help enterprises implement FAT processes more efficiently.
As industries evolve, FAT will continue to play a pivotal role in quality assurance, leveraging digital tools and global collaboration to meet the demands of modern manufacturing.